If you run a fabrication shop, steel mill, or any operation that relies on profile machines to cut, punch, or shape structural steel, aluminum, or other metals, you know how critical these workhorses are to keeping production on track. As a profile machine supplier who’s spent 18 years installing, troubleshooting, and maintaining these units for shops across North America, I’ve seen firsthand that a well-maintained profile machine isn’t just more reliable—it also delivers cleaner cuts, less waste, and lower long-term costs than one that’s ignored. Too many operators treat maintenance like an afterthought, waiting until a breakdown shuts down a job instead of building a routine that catches small issues before they turn into expensive repairs. In this post, I’ll break down the maintenance steps I share with every customer who buys a profile machine from us, from daily quick checks to annual deep dives, so your equipment stays productive for decades. Profile Machine
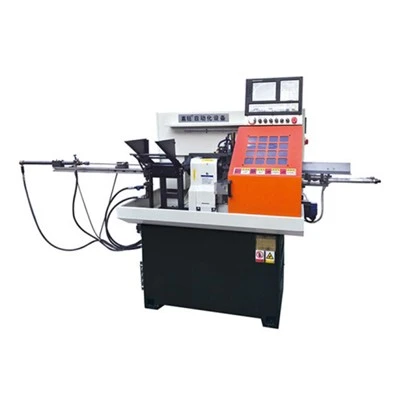
Daily Routine: 15 Minutes That Prevent 80% of Breakdowns
Most of the serious problems we see start with skipped daily checks. I tell customers to block 15 minutes at the start of each shift to go through these steps—no exceptions. First, inspect the cutting head and tooling. Look for nicks, burrs, or chips on the end mills, drills, or plasma cutters you use. A damaged tool doesn’t just give a rough cut; it can put extra stress on the machine’s spindle or torch mount, leading to misalignment over time. If you use plasma, check the electrode and nozzle too: even a small amount of spatter built up on the nozzle will reduce cut quality and force the machine to work harder. Wiping spatter off with a copper brush (not a steel one, which can scratch and contaminate parts) takes 30 seconds and saves you from having to replace a $50 nozzle every week instead of every few months.
Next, check the coolant level for your cutting systems and the lubrication reservoir. For machines with liquid-cooled spindles, low coolant can cause overheating that warps the spindle bearing—a repair that costs thousands of dollars and takes days to complete. I keep a spare jug of the manufacturer-recommended coolant on every customer’s service truck, and I tell them to do the same: never use tap water, which has minerals that corrode lines and clog filters. For lubrication, most profile machines use automatic oilers for the linear rails and ball screws. A quick glance at the oil level indicator should show it between the “min” and “max” lines. If it’s low, top it off with the correct viscosity oil—using the wrong weight can cause friction that wears out rails prematurely.
Finally, do a visual check of the machine’s frame and worktable. Look for any loose bolts around the cutting head, or small dents in the worktable that could cause stock to shift during a cut. A $2 Allen wrench and two minutes tightening loose bolts are way easier than stopping a mid-job to reposition a warped part. I once had a customer who skipped this check and ended up with a $12,000 part ruined when a bolt on the y-axis came loose and shifted the cutting head. That loss could’ve been avoided with 60 seconds of prep.
Weekly Maintenance: Dive Deeper to Extend Part Life
Weekly checks add about an hour to your schedule, but they’ll extend the life of your machine’s most expensive parts by 2–3 years, on average. Start with the linear rails and guideways. These are the components that the cutting head slides along, and they rely on a consistent layer of lubrication to prevent metal-on-metal wear. Most shops just let the automatic lubricator do its job, but once a week, wipe down each rail with a clean cloth and apply a thin coat of grease made for linear motion components. Don’t over-grease it—too much grease will attract metal shavings, which act like sandpaper and scratch the rail surface.
Next, clean the air filter if your machine uses pneumatic components (common for clamping systems or tool changers). A clogged air filter reduces pressure, which can cause clamping arms to slip or tool changers to fail mid-operation. To clean it, remove the filter from its housing and blow it out with compressed air (keep the pressure below 80 PSI to avoid damaging the filter). If the filter is discolored or torn, replace it immediately—we stock spare filters for every machine we sell, so customers never have to wait for a part.
Also, check the machine’s electrical connections. Open the control panel and look for any loose wires or signs of dust buildup. Dust is a big enemy here—it can cause short circuits or overheat circuit boards. Use a low-pressure air compressor to blow dust out of the panel, and tighten any loose terminal screws with a screwdriver. I’ve seen too many machines go down because a loose connection on the spindle motor caused intermittent power loss—something that’s easy to fix with a quick check.
Monthly Tasks: Alignment and Calibration for Precise Cuts
Alignment is where a lot of operators slip up, and it’s what separates a profile machine that cuts accurate parts from one that wastes material. Once a month, calibrate the machine’s axis alignment. For most modern profile machines, you can use a digital alignment tool or even a simple square to check if the x, y, and z axes are perpendicular. If you notice the cut is off by a few millimeters, adjust the calibration settings in the machine’s control software—most units have a built-in calibration wizard that walks you through the steps. Skip this, and over time, the machine will drift, leading to parts that don’t fit together correctly on your job site.
Also, test the emergency stop (E-stop) button. This is a safety critical part that’s often forgotten until it’s needed. Press the E-stop to make sure it cuts power immediately, then release it and reset the machine. If it doesn’t respond, check the wiring or call a service technician—don’t risk using a machine with a faulty E-stop. I’ve had customers who ignored this check and had a near-miss when a cutting head started moving unexpectedly; the E-stop failed, and they had to shut down production for three days while they fixed it.
Finally, inspect the drive belts for your axis motors. Belts stretch over time, which can cause the cutting head to move inconsistently. If you notice slippage during a cut, tighten the belt tensioner according to the manufacturer’s specs. If the belt has cracks or fraying, replace it before it breaks mid-job. A $50 belt is way cheaper than stopping production to replace a broken one.
Quarterly Maintenance: Coolant and Filter Replacements
Coolant and filters are easy to ignore, but they’re vital for keeping cutting systems running smoothly. Every three months, drain and replace the coolant in your spindle and plasma cooling systems. Old coolant gets dirty, which reduces cooling efficiency and can cause corrosion in the lines. When you replace it, flush the system with distilled water first to remove any buildup—this ensures the new coolant works properly. Also, replace the coolant filter at the same time; a clogged filter will reduce flow and cause overheating.
For the machine’s hydraulic system (if you have one for clamping or heavy cutting), check the hydraulic fluid level and color. If the fluid is dark or has metal shavings in it, drain and replace it and the filter. Old hydraulic fluid can cause clamps to weaken, leading to stock shifting during cuts. I once had a structural steel shop that skipped this and ended up with a beam cutting wrong, costing them $20,000 in rework. It’s a small, quarterly task that saved them from a major loss.
Also, check the torch height control (THC) for plasma machines. The THC keeps the torch at the correct distance from the metal, which is essential for a clean cut. Test it by cutting a sample piece of metal and checking the kerf (the width of the cut). If the kerf is uneven, adjust the THC settings or clean the THC sensor. A dirty sensor will give wrong readings, leading to bad cuts and wasted material.
Annual Deep Maintenance: Prevent Catastrophic Failures
Once a year, schedule a full deep maintenance check, either with your in-house team or a service technician from our company. This is the time to do the tasks you don’t have time for during regular shifts. First, completely disassemble and clean the linear rails and ball screws. Remove the rails from the machine, clean off all old grease and metal shavings, and inspect for wear or damage. If the rails have minor scratches, you can polish them with a fine-grit sandpaper (as long as it’s not deep enough to cause alignment issues). If the ball bearings are worn, replace the ball screws—this is a big job, but it’s cheaper than replacing the entire machine.
Next, inspect the spindle motor for wear. For machines with a mechanical spindle, check the bearings for play by wiggling the cutting head from side to side. If there’s more than a small amount of play, the bearings are worn and need to be replaced. For plasma spindles, check for arcing or unusual noise—both signs of a failing motor. I recommend replacing spindle bearings every 5–7 years, depending on how often you use the machine.
Also, update the machine’s control software. Modern profile machines have software that gets updates to fix bugs, improve cut quality, and add new features. Our team sends free software updates to all customers, and annual maintenance is the perfect time to install them. Outdated software can cause slow performance or even compatibility issues with new tooling.
Finally, do a full safety inspection. Check all guards, limit switches, and safety interlocks to make sure they’re working correctly. Replace any worn guards, which are there to protect operators from flying metal shavings. Safety should never be an afterthought—we design our profile machines with multiple safety features, but they only work if you maintain them.
Pro Tips From 18 Years in the Profile Machine Business
After working with hundreds of customers, I’ve picked up a few tricks that make maintenance easier. First, keep a maintenance log. Jot down each day’s checks, any issues you notice, and when you replace parts. This log helps you spot patterns—like if your air filter needs replacing every two weeks instead of four, which could mean a leak in the line. It also makes it easier to plan for future parts and service.
Second, use genuine replacement parts. It’s tempting to buy cheaper aftermarket parts, but they’re often made with lower quality materials that wear out faster. We only sell OEM parts for our profile machines, and I tell customers that spending a little more on a genuine end mill or belt saves you from replacing it every month instead of every six months.
Third, train your operators on basic maintenance. A machine operator who knows how to check oil levels or clean a nozzle is way more likely to catch a small issue before it becomes a big one. We offer free operator training for every machine we sell, and I always spend extra time going over maintenance tips because I know it’s the key to long-term performance.
Final Thoughts

Maintaining a profile machine doesn’t have to be complicated. It’s all about consistency—those 15-minute daily checks, the weekly and monthly tasks, and the annual deep dive. Skipping maintenance might save you time in the short term, but it will cost you way more in repairs, reworked parts, and downtime when your machine breaks down unexpectedly. Our team works with customers every day to make maintenance as easy as possible—we stock spare parts, offer phone support for quick troubleshooting, and can send a technician to your shop for annual checks. If you’re looking for a reliable profile machine that’s built to last, or you have questions about maintaining the one you already have, get in touch with our team today to discuss your needs and find the right solution for your operation.
Vertical Machining Center References:
- "Industrial Metalworking Equipment Maintenance Best Practices" – Association for Manufacturing Technology, 2022
- "Guide to Linear Motion System Care and Lubrication" – Thomson Industries, 2021
- "Plasma Cutting Machine Maintenance: A Step-by-Step Manual" – Hypertherm, 2023
- "Structural Steel Fabrication Equipment Maintenance Checklist" – American Institute of Steel Construction, 2022
Taizhou Qiyang Trading Co., Ltd.
As one of the most professional profile machine manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy bulk profile machine for sale here and get quotation from our factory. Customized orders are welcome.
Address: Zhenhai Village, Binhai Town, Wenling City, Taizhou City, Zhejiang Province
E-mail: qycncmachine@outlook.com
WebSite: https://www.qycncmachine.com/
